Tuesday, January 31, 2017

Project #12 - 180 mm gyuto in Niolox steel

The time has come for the to try a steel that is not all that well known outside Europe  - the Niolox also known as SB1. It was brought to the attention of knifemaking community by Jürgen Schanz who also himself is a knifemaker and experienced metallugist. He also sells knife supplies and offer heat treatment services. In other words - I have the chance to have my stainless blades heat treated by someone who has very detailed knowledge of the steel and lot of experience how to get the most out of it.

The Nilox is supposed to be similarly to AEB-L a very fine grained steel. The Niobium forms very small and very hard carbides what allows the steel to be fine grained and resist abrasion well. In other words a very interesting steel (not only) for kitchen knives.

At some point in the future I would like to compare it to AEB-L and D2 (which has usually much larger grain structure) - actually - that is what Project #13 will be all about :)

The design

For the testing purposes I have decided to make a smaller knife. At the moment I plan a simple WA handle, but may even give a hidden tang western handle a try.

The design of the blade was simply done by hand on paper on my bus commute. I am actually really starting to enjoy designing blades by hand.

The knife will be made of 2.2 mm thick (thin!) steel. The blade will have a continuous convex grind and I plan to make it nice and thin behind the edge.

The blade

I took a fresh blade for the hack saw and had the coarsely cut-out blank it under 10 minutes. Part of that was of course that the steel was only 2.2 mm thick. Still - this would have taken longer with a steel like D2.

20 minutes later the blank was shaped, edges ground up to #120 grit (I used cheap #40 ceramic belt to shape the blank) and thus basically ready for grinding the bevels.

You may notice that the bump where the tip of the blade is supposed to be. I have seen Don Nuygen doing this and realised how a great idea that was. This makes the tip more robust while grinding, heat treating and final shaping after HT. The bump also serves as heat dump when final shaping after HT. I will see how that will work for me.

The design and the blade blank. Notice the hump ner the tip.
The grinding was fairly fast - this is partially because of the thin stock and it would also seem that the steel is relatively easy to grind, even though it seems that it dulls belts quickly. The grind is a relatively flat convex with a little more curve close to the edge. I hope to get usable food release with this knife. We shall see how that will work. As usually I ground the bevel, then ground the distal taper and blended these two together. But I have to admit that I do not yet have a better defined procedure yet and I was jumping between the two until I felt the blade was about right.

As always - I was checking the thickness at the edge and at 5, 10 and 20 mm behind the edge and tried to keep it as consistent as possible with slight taper towards the tip.

Pre-HT grind.

Blade ground (pre HT) and cleaned up to #240 belt
Once the blade was ground I moved to the tang. Since this was going to be a fairly thin and lightweight knife I opted for the tang height of 10 mm (I use 12 mm on larger knives). I have used a filing guide and reshaped the tang with a belt grinder. The shoulders do not need to be quite as perfect as I planned a conventional WA-type handle and no metal bolster.

Sanding the tang to shape.

Tang finished.
 Before the blade was sent to HT I have it a quick finish with #240 and #400 sand paper. Not quite perfect yet - this is the area I need to improve my speed/efficiency as well as the final result.

Sanding the blade to #400. I write down the note if I do not manage
to finish in one session.
Once back from HT it was time for final grind. There was not all that much left to grind apart from close to the cutting edge. and once the grind was finished to profile the tip.

Blade after HT after first few passes on #120 Norton Blaze belt.

Detail of the grinding on the cutting edge.
Once the blade was ground and the tip profiled, I continued with 3M Trizact 'gator' Belts (A100, A65 A30) to refine the finish and with the flexible 3M Trizact (A30) for the last clean-up on spine and choil.

Note: Here I would like to mention that my blade grinding procedure is far from fine tuned and I am still learning what belt progression works the best for me, so take the above just as an example.

In Parallel I have started to work on the handle. I chose Mora for the bolster and Bocote body of the handle with yellow and black fibre spacers. The main reason to choose these materials (other than design) was that they are relatively lightweight. The blade is very thin and I did not want the knife to be butt-heavy.
Blade before finishing and handle materials.
The making of the handle was relatively straight forward. I would cut a piece of Mora for the bolster and squared it up, cleaned and squared up the Bocote, cut out the fiber spacers and glue it all together with a G/flex epoxy.

Future-to-be bolster.

Once the glue cured I used first belt and disc sander to clean and square up the block. The challenge here was to remove as little material as possible before the next steps, as both woods were on the thin side and there was very little room for error.

Squared up handle ready for drilling.
The handle was subsequently drilled (10 mm) a dowel was made out of beech. I always make it a few mm longer so I can minimise the damage to the front of the dowel while final fitting. I cut the slot in the dowel with a hacksaw and then used belt sander to widen it until the tang fits. It pays to be careful here - the better fit the easier putting the knife and handle together. I also sand the dowel lightly from outside, so that it can be fit in the drilled opening (with the tang in the slot) with only very little resistance. Once covered in epoxy, the fit will be tighter and the epoxy will also tend to push the two halves of the dowel together.

Ready to glue the dowel.
I mixed the glue (G/flex has 45 minutes pot time, so no hurry is needed) cover the dowel with a thin layer of glue. I insert the blade - that makes it easier to get the angle right. I use a thin piece of steel (and off-cut from a blank) and sue it to make sure that there will be no gaps between the bolster and the dowel.


Once the glue cures I would do some light rasping with a needle rasp to get the tang fit cleanly - some glue usually leaks in the slot and needs to be removed.

... and if you hurry you will brake your brand new needle rasp ...
The handle will soon proceed to final shaping, but let's do some blade finishing first. Since I managed to get acceptable finish on the belt sander, I could start with a #400 grit sandpaper. The side of the blade facing down is completely covered with an orange Tesa tape (the best I found so far - leaves practically no residue)

It turned out that Niolox reacts quite differently to sanding than the D2 (the only other stainless steel I have used so far). When I went up to #600 grit I started to get a quasi-mirror finish, but at the same time I was seeing quite some #400 scratches I could not quite get out. So I went back to #400 and finished the blade with this grit.

Working with a #400 sanpaper - there are still grinding marks to be removed.
Back to the handle. I cleaned all sides on disc sander, and then squared up on #160 sandpaper.

Finishing the shaping before chamfering.


Flattening all sides.
The most critical part of the process for me (because I do it on the disc grinder) is to chamfer the handle to octagonal shape - I find it very important not to try to hurry as it is very easy to slip or grind too much away.
Chamfering to octagonal shape.

Testfitting the blade. Good!
Once the final shaping of the handle is finished it is time to finish the surface. I go through progression of #240, #400, #600 and #1000 sandpaper. The step with #240 is done on flat support - all scratches left by the disc grinder needs to be removed.

Note: One needs to be careful and watch where the pressure is applied as one may unwillingly 're-shape' the handle. Ask me how I know.

Sanding with the higher grits is done with a small sanding block (about 10 x 2 x 4 cm) - the long narrow sides have a double-sided scotch tape so that I can swap the paper. I do the sanding 'free hand'.

Hand sanding - finishing the handle.


Hand sanding finished.


Hand sanding finished.
Once the sanding was finished all that the handle needed was a few coats with a board butter and it was finished.

Oiled with board butter.
Once the handle was finished I glued it onto the knife with G/flex epoxy. That is a slow procedure in particular when it is colder in the shop and the glue does not want to flow quite as fast as I would like, plus it takes patience once the knife was fully inserted to take out all bubbles that may appear many minutes later.

As the photos of the finished knife show - I have one obvious need for an improvement. namely when putting the edge on the blade for the first time I inevitably scratch the blade 5mm or even more from the cutting edge meaning that the blade should actually be re-finished again. Hmmmm, I need to give it some thought.

Finished knife

Since I was in a hurry and the finished knife was already with my friend for testing, I did not manage to take some photographs, so here are a few taken by my friend.

Looking at the photos below I can not help but admit that the finish of the blade does look a bit ... particular (the photos do make it look a bit more scratchy than in person though). I really need to work on it in the future.


Sunday, December 25, 2016

Project #16 Handle for Watanabe Mukimono

This project was commissioned at the same time as the project #15, but here I was given a 'free hand' on the handle materials and design. I could not resist to try something new - see below how did that work out :)

The knife in questions is a small mukimono made by Shinichi Watanabe. It had a 'standard' burned chestnut D shaped handle and so the handle removal was very simple, since these are not glued on, but just burned-on the tang.

Design & Materials

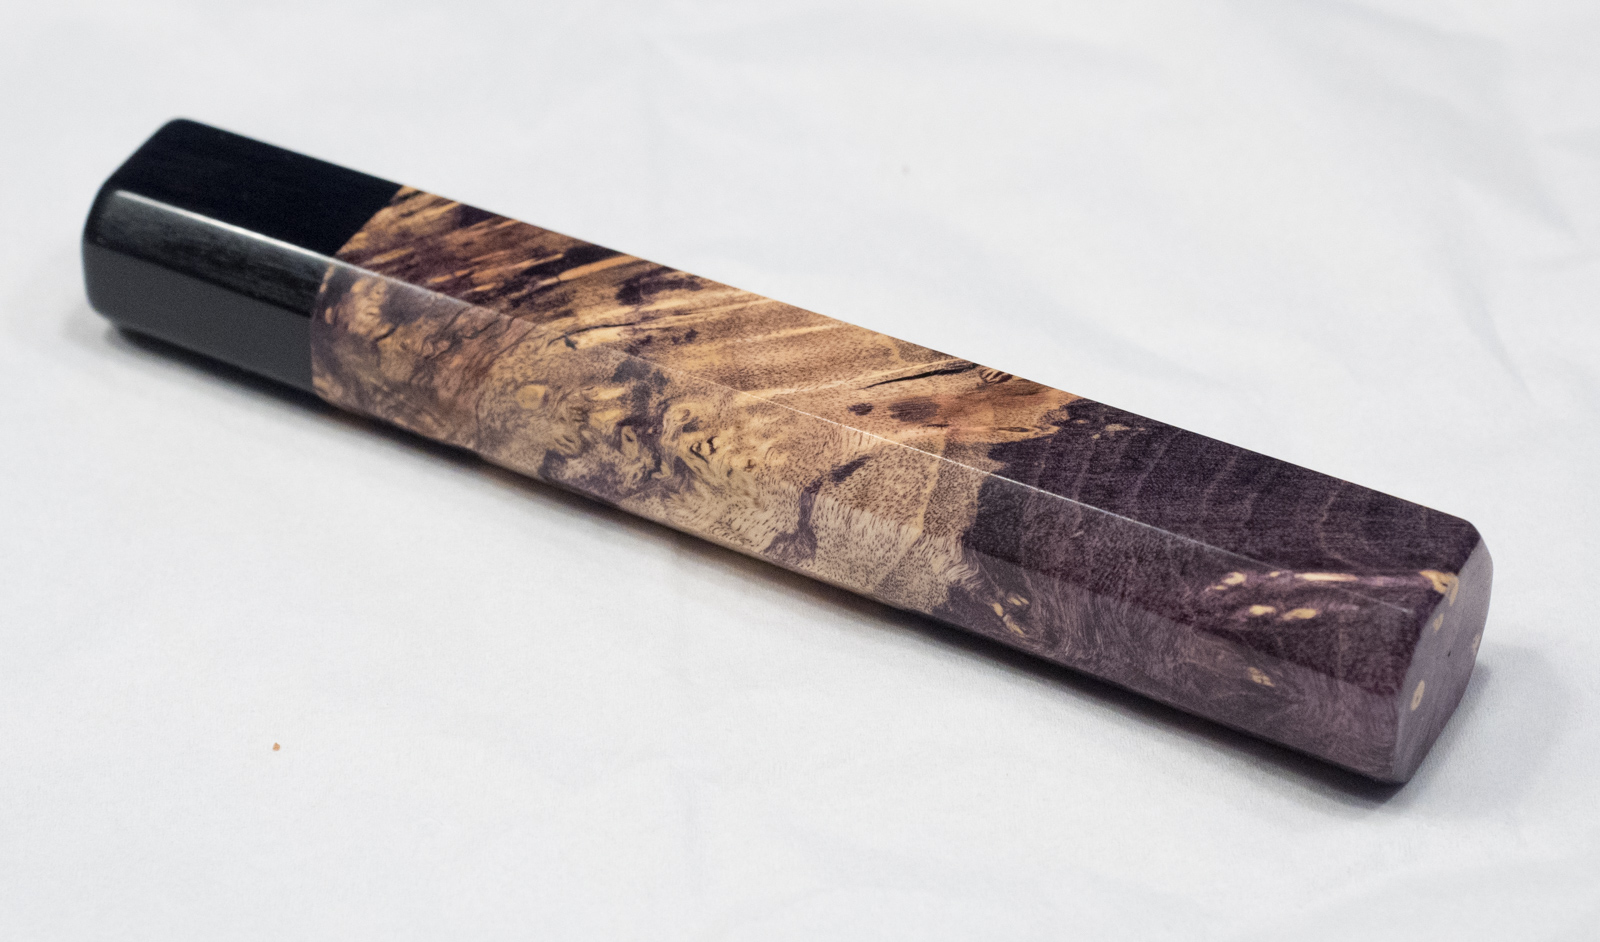
For a long time I have concentrated only on natural woods, but I was always attracted to dyed materials. I have recently bought a few blocks from different sources and this handle was a good opportunity to test one of them.

I have also wanted to try water buffalo horn (a 'standard' ferrule material on traditional Japanese handles) as well as some metal spacers. So the final selection was:
  • stabilized & dyed maple burl (from stabwoodlab)
  • water buffalo horn
  • black fiber paper spacers
  • 1 mm thick nickel silver spacers

Starting point - original handle and materials for the new one.

The handle block

Before I did the easy part - square the wood up, clean the gluing side of the horn, cut the pieces of fiber paper and nickel silver and glue them all together - I considered different options on how to deal with the fact, that there are metal spacers that need to be drill in some way. 

  1. One option would have been to drill all components beforehand and glue them directly with a dowel (that would not have a tang slot at that point) and then drill the tang slot afterwards. Doable, but because of the thinness of the blade the making the tang slot would have been a lengthy job.
  2. I have decided to go with second option - glue all the components together and do the drilling afterward. I will discuss the pluses and minuses later. I have used BladeBond Ultra epoxy for the first time here (will be relevant below).
  3. Third option that did not come to my mind would have been to drill the holes in the horn, nickel silver, fibre paper and a shallow hole in the wood, than make a shot (1 - 2 cm) dowel from soft wood that would only serve to align all the parts and would be later drilled-through with the same drill bit to allow to mount a slotted hardwood (beech) dowel.

About to glue it all together.

Gluing the handle block
Ready for the next step.

Glue excess ground off, ferrule shaped to align with the rest of the block.

Once the handle was glued I cleaned the block up (remember, it was already squared up before gluing) and drew centre lines on all sided, top and bottom. I also gently tapped the bottom to keep the track of where the centre was.


After all lines were drawn I realized that I forgot to square-up the bottom of the handle. The point of doing so was to make alignment in the vice for drilling easier.

Squaring up the bottom side of the handle.

Drilling the opening for the dowel

Note: Since I did several unfortunate choices in this part of the process, I have decided to describe it in more detail.

As mentioned above - I have decided to do the drilling after all the components were glued together. The main issue to deal with were of course the metal spacers. Even though not too thick, these still needed to be drilled with different drill than the one I normally use (drill bit for wood with the guiding 'tip').

I have first drilled a 'normal' hole with 10 mm diameter (first mistake, I should have started with a much thinner drill bit and use the hole in the horn as guide while drilling through the metal spacers) with the drill bit for wood and swapped to a drill bit for steel (second mistake - apparently not a really sharp one) once I reached the metal spacers.

Starting to drill - so far so good.

I have underestimated (third mistake) the amount of heat that will be produced while drilling through the nickel silver spacers. When I was half way through the first spacer I noticed that the handle block is loosing its mechanical stability and a few seconds later the horn cleanly delaminated from the rest of the block. Bummer :(

And the ferrule went clean-off when the drill bit
touched the first spacer.
Just drilling a little more to see how the metal spacer holds on the
underlying fiber spacer. Poorly.

Close inspection showed that the glue detached from the surface of the nickel silver (which I cleaned with acetone, but - fourth mistake - forgot to roughen with sanding paper and left it glossy polished).

Checking out the second nickel silver spacer which was sandwiched between to fibre paper spacers showed that this one was already delaminating, even though it had seen only a very short drilling (just the tip of the drill bit). I was able to detach it from both fibre spacers - again - there was no glue left on its surface.

There is not glue attached to the nickel silver. The scratchy spots are
from flattening with a hammer prior to gluing.

At this stage I should mention that I have used the BladeBond Ultra epoxy (a dedicated epoxy for knifemaking) which I did not test before with the materials in question (fifth mistake - untested glue). Afterward I have used the G/flex with the two spacers just to see how they will hold and looked fine, but I did not try to drill them.

So to save what still could be saved I sanded the remaining fibre spacer off the wood, sanded both wood and horn and glued them together.


Handle shaping

Once the glue cured I have proceeded in the standard way. I prepared a dowel from a 10 mm round beech, cut the tang slot with a hack saw, widened it with a belt sander and #120 belt until it would fit well on the tang and glued the dowel inside the handle block with the G/flex epoxy (wood glue would have worked as well). I have briefly inserted the tang inside and made sure that the blade is under right angle against the upper and lower side of the block. Indeed - a slight rotation could be corrected later, but it makes your life simpler if you do not have to correct this.

Note: Do not use too much glue for the dowel, as it will find its way inside the slot and you will have tough time to file it away so that you can fit the tang inside later.


Once the dowel fits the blade and also the hole in the block
(without too much resistance) it can be glued it. 
Checking handle alignment relative to the handle block after gluing.

Once the dowel was glued it was time to proceed with rough shaping. But before I would do that I would use a thin needle rasp (which I flattened from one side with a belt grinder to be able to sand tang slots as thinner than 3 mm) and make sure that the blade tang would fit in nicely. Then I would mark the handle with a pencil on the sides of the handle, grind off the excess of the material with a sharp coarse #40 belt, clean up on the disc grinder and do the same for the remaining two sides.

Note: If you are not sure about what size the handle should have when finished, then keep do this in a few steps. Ideally you would get the idea on the size from some other existing handle, as at this stage you can not really test how the handle feels in hand. 

Rough shaping the handle.

Rough shaping finished - cleaning up on a disc grinder.
Once the rough shaping was finished I used #240 sanding paper to flatten all sides (I can not really get perfectly flat grind on my disc sander because it is really small before I would go back to the disc sander and grind the handle to octagonal shape.

Flattening the handle before giving it octagonal shape.

Final shaping is one of the sensitive steps - I am doing it 'free hand' with the disc sander. I first try to get a reasonable angle, grind just a bit and move to the next 'corner' and work on all sides iteratively until I like the result. The reason for this is that it is rather easy to make a mistake and grind under wrong angle. Since this work does not take that much time, I really recommend not to hurry this step.

Final shaping finished - next step is handle finishing.

Once the octagonal shape of the handle is finished, I take the handle to #240 sand paper attached to sanding stone and make sure that all 8 facets are flat and I have removed all the scratches left by the disc grinder.

Note: Be careful here. #240 sandpaper is still fast enough and if you use too much pressure you can easily remove considerably more material than you have planned. Make sure that you apply the pressure evenly left-right and front-back as otherwise you will chance the angle of the facet you are sanding.

The wide facet has the longitudinal scratches from the hand sanding,
the narrow one has still the disc sander finish.

Once the handle is clean I move to sanding with a small hard wood block ( ca 20 x 60 x 100 mm ) with a double-sided Tesa scotch tape on the narrow long sides which I use to attach different sanding papers. I follow with 400, 1000 and 2000. At each step I round the edges on the ferrule and sand under constant angle the edges on the opposite end.

After #2000 grit sanding paper.

After #2000 grit sanding paper.

After #2000 grit sanding paper.
Normally I would stop between #600 and #1000 grit, but wit this handle material both the horn and stabilized wood seemed to need a finer finish. So I moved to micro mesh pads and went from #2400, #3200, #4000, #6000 and #8000. I was a bit surprised to see that the horn did not want to reach a deep polish. It turned out (in direct comparison with several Japanese handles I have) that horn has its own structure and the fine grooves were filled with very fine wood dust what made the impression of deep scratches even stronger. Cleaning the handle and wiping it with board butter made it look much nicer.

Note: contrary to sanding paper which can be mounted on hard surface to have a well defined sanding surface, the micro mesh pads are soft. This inevitably means that there will be tendency to round over edges and the only control you have is how long you will be sanding with the pads.

After micro mesh treatment.

After micro mesh treatment. See the dust filled grooves on the ferule?

Once all the sanding was finished the handle was treated with a board butter.

Finished handle.
Finished handle.
Finished handle.
Finished handle.
Finished handle.
The only work left to do was the glue the handle onto the tang. I have used the G/flex epoxy which is fluid enough to (albeit slowly) flow inside the narrow tang slot. At the same time the glue as 45 minute pot time, so you do not need to hurry and once you get the blade in place you have still time to clean all the glue from the blade and the handle.

Getting ready for the final gluing.
Blade is in place, everything was cleaned and looks good :)

Lessons learned

  • Test the process first - see my problems using the BladeBond Ultra epoxy to glue the nickel silver spacers. I suppose this is a mistake on my side (see the test of this glue by Walter Sorrells on YouTube)
  • If you are using a new concept for the first time - think it through before you execute it. I did not and at the end I got lucky. I will proceed differently next time.
  • Be careful when hand sanding (cleaning up & flattening) the facets of the handle with coarse or medium grit sandpaper - you may remove more material than you expect.
  • Even if you have full contact of the flat area with the sand paper, the material will be removed there, where you apply pressure.
  • I have used here a new source of stabilized wood (from the xx642011 on eBay - also know as stabwoodlab on Instagram) . It turned out to be of good quality, but should that not be the case, I would 'only' have to make a new handle from a different material. I would have not used material of unknown quality if the handle design would have required to shape the handle after it was glued on the tang.

Finished handle